When you click on links to various merchants on this site and make a purchase, this can result in this site earning a commission. Affiliate programs and affiliations include, but are not limited to, the eBay Partner Network.
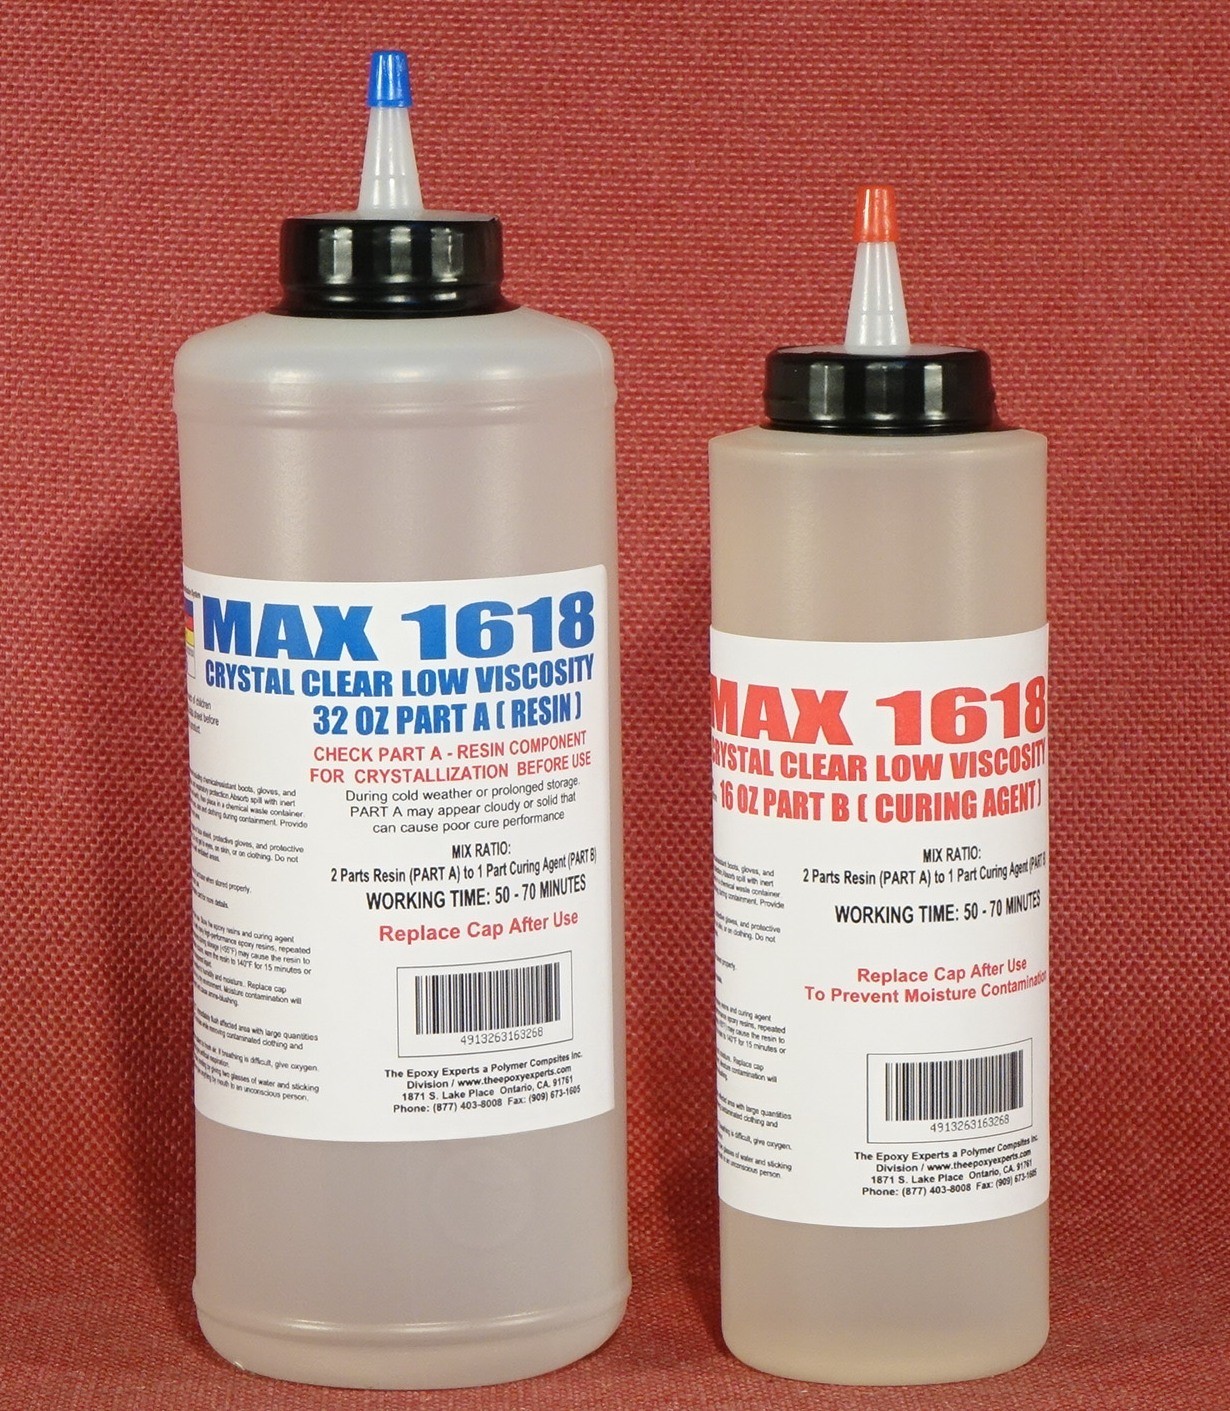
MAX 1618 A/B
CLEAR IMPREGNATING RESIN FOR COMPOSITE FABRICATION
Compatible With
Fiberglass, Carbon Fiber, Kevlar, Basalt, Quartz
(48 Fluid Ounce- 1.5 Liters Combined Volume)
1 Quart Part A And 1 Pint Max 1618 Part B
PRODUCT DESCRIPTION
MAX 1618 A/B is our lowest viscosity (very thin mixed consistency) high-performance epoxy resin system. It is designed as an impregnating resin for making carbon fiber composites for vacuum infusion, RTM, VARTM, and hand lay-up process. MAX 1618 A/B also works well with other types of composite fabrics such as fiberglass, Kevlar, Texalium, aramid, nylon, quartz, and hybrid woven fabrics.
MAX 1618 A/B is mixed 2:1 mix ratio by weight or by volume and exhibits a very low initial viscosity, good wetting, air bubble release, and provides up to 60 minutes of working time up to 200 gram mass at 75°F (24°C).
The mixed viscosity, working time, and full cure time are governed by temperature. During the cold season, the consistency will be higher in viscosity and slow to react and longer cure times. Warming the resin and curing agent to 75°F (24°C) before mixing the PART A and PART B compensates the effects of cold temperature and maintains its working time and full cure time. Prewarming the components also minimizes air bubble entrapment during blending and lay-up by lowering the viscosity.
MAX 1618 A/B cures tack-free after 6 hours and develops green-strength after 12 to 18 hours. It fully cures in 24 to 36 hours at 75°F (24°C).
For faster processing, MAX 1618A/B can be heat cured for 4 hours at 220°F.
20 Plies Of Carbon Fiber Vacuum Bagged Laminate
3 Layers Of Carbon Fiber 2x2 Twill Laminated With MAX 1618 A/B
3 Plies Carbon Fiber Laminate -180 Degree Flex Without Cracking
100% Carbon Fiber Hood With MAX 1618 A/B
General Principle Of Vacuum Bagging
General Principles of Vacuum Bagging With MAX EPOXY RESINS - YouTube
Video will open in a new window
MAX 1618 A/B VACUUM INFUSION MOLDING PROCESS
CARBON FIBER VACUUM INFUSION WITH EPOXY RESIN - VACUUM BAGGING WITH MAX 1618 EPOXY RESIN - YouTube
Video will open in a new window
Note The Absolute Clarity Of The MAX 1618 A/B Specimen Exhibiting Excellent Transparency
Common epoxy-based formulations engineered for high-strength structural applications typically exhibit very poor color stability due to the use curing agents that are inherently yellow or amber in color. In contrast, resin formulations engineered for transparent clear and other aesthetic applications yield lower mechanical strength caused by the use of lower functionality amine curing agents.
MAX 1618 A/B does not utilize any liquid plasticizers and accelerators such as nonylphenol or benzyl alcohol, which causes extreme yellowing even if the cured polymer is protected or unexposed to Ultraviolet or ambient heat.
THIS KIT INCLUDES A SET OF YORKER CAPS FOR CONTROLLED DISPENSING.
Use these Yorker caps to dispense the material with ease and minimize over pouring and reduce spills. We do not recommend using
dispensing pumps. The curing agent or part B of any epoxy resin system is sensitive to moisture and carbon dioxide, which will react with the curing agent and form carbamate crystals (salt-like crystals that form on the tip of the pump) and reduce reactivity.
*
RESIN CRYSTALLIZATION FROM PROLONGED STORAGE OR COLD WEATHER EXPOSURE
The resin component or the PART A may crystallize due to cold temperature exposure.
Please inspect the resin component for any solidified crystals which will appear as waxy solid or cloudiness on the bottom of the PART A bottle.
An information postcard is included with each package.
View the following video for identification and processing.
DO NOT USE UNLESS PROCESSED TO REVERT ANY CRYSTALLIZED RESIN BACK TO A LIQUID STATE AND AVOID POOR CURED RESULTS.
Celsius To Fahrenheit Conversion
Physicaland Mechanical Properties
Heat Resistance StudyBy Shore Durometer Hardness Test
The heat resistance of MAX 1618 A/B was tested by heating a 2-inch cube in 5-degree increments and the Shore hardness was determined using both the Shore A and D scale. This test demonstrates the heat resistance of the MAX 1618 A/B by determining at what temperature the Shore Hardness reading dramatically change. At 140°F, a considerable change in Shore D Hardness Scale occurred due to the sharp needle-like indenter of the equipment began puncturing the surface of the specimen which may make the Scale D Hardness an unreliable test data.
The Shore A scale demonstrated a dramatic change in hardness at 240°F which demonstrates it maximum heat tolerance more accurately than the Shore D scale.
Hardness
Application
30 Shore A
Art gum erasers
35 Shore A
Rubber bands
40 Shore A
Can tester pads
50 Shore A
Rubber stamps
55 Shore A
Pencil erasers
60 Shore A
Screen wiper blades
65 Shore A
Automotive tires
70 Shore A
Shoe heels
75 Shore A
Abrasive handling pads
80 Shore A
Shoe soles
85 Shore A
Tap washers
90 Shore A
Typewriter rollers
95 Shore A
Fork lift solid tires
60 Shore D
Golf ball
70 Shore D
Metal forming wiper dies
80 Shore D
Paper-making rolls
Shore hardnessis a measure of the resistance of a material to penetration of a spring-loaded needle-like indenter.
Shore Ascale is used for testing soft elastomers (rubbers) and other soft polymers.
The hardness of hard elastomers and most other polymer materials is measured byShore Dscale.Shore hardness is tested with an instrument called Durometer. Durometer utilizes an indenter loaded by a calibrated spring.The measured hardness is determined by the penetration depth of the indenter under the load.Two different indenter shapes and two different spring loads are used for two Shore scales (A and D).
The loading forces of Shore A: 1.812 lb (822 g), Shore D: 10 lb (4536 g).
Shore Hardness value may vary in the range from 0 to 100. Maximum penetration for each scale is 0.097-0.1 inch.This value corresponds to minimum Shore hardness: 0. Maximum hardness value 100 corresponds to zero penetration.
MAX 1618 A/B COLORSTABILITY COMPARISON
Note The Absolute Clarity Of The MAX 1618 A/B Specimen Exhibiting Excellent Transparency
Clear epoxy systemsformulated using plasticizers and accelerators such as the specimen.
The left specimendemonstrates poor color stability even if it is unexposed to direct sunlight orelevated temperature.Note the MAX 1618 specimen that was formed at thesame time and kept in a temperature controlled (25.0°C +/- 0.5 °C) chamber that filtersout any UV radiation from an ambient light source.
Competitive (1:1 Mix Ratio) Brand Clear Resin System After Sunlight Exposure
COATING AND CASTINGMEASUREMENTSANDSTANDARDS
FLUID GALLON VOLUMECONVERSION
1 US GALLON
231 CUBIC INCHES
1 US GALLON
128 FLUID OUNCES
1 US GALLON
3.7854 LITERS
1 US GALLON
4 US QUARTS
1 US GALLON
16 CUPS
1 US GALLON OF UNFILLED PURE EPOXY RESIN
9.23 POUNDS
1 US GALLON OF UNFILLED PURE EPOXY RESIN
4195 GRAMS
EPOXY RESIN MIXINGTECHNIQUE
The use of a weighing scale to measure out the resin and curing agent is highly recommended to ensure proper cured performance.
This digital scale is available for purchase by clicking the link below.
Purchase this scale with any of ourproduct offering and the shipping cost of the scale is free.
Please View The Following Video For The Proper Mixing Of Epoxy Resins.
It Demonstrates The Proper Technique Of Mixing Any Type Of Epoxy Resin System.
The Proper Cure And Final Performance Of Any Epoxy Resin System Are Highly Dependent On The Quality And Thoroughness Of The Mix.
The Resin And Curing Agent Must Be Mixed To Homogeneous Consistency.
Improper mixing is the most common cause of tacky spots or uncured resin to appear on the surface.
Please View The Following Video Demonstrations To Ensure A Trouble-Free Curing With Any Epoxy Resin System.
How To Mix Epoxy Resin For Food Contact Coating. Avoid Tacky Spots, Minimize Air Bubble When Mixing - YouTube
Video will open in a new window
Using the App? Paste link into a browser window:
[isdntekvideo]
AIR BUBBLE REMOVAL TECHNIQUE
HOW TO REMOVE AIR BUBBLES
Video will open in a new window
CUTTING AND POLISHING
Video will open in a new window
POLISHING
The Following Are Suggested Processing Information For
COMPOSITE FABRICATING BASIC GUIDELINES
By resolute definition, a fabricated COMPOSITE material is a manufactured collection of two or more ingredients or products intentionally combined to form a new homogeneous material that is defined by its performance that should uniquely greater than the sum of its individual parts. This method is also defined as a SYNERGISTIC COMPOSITION.
COMPOSITE MATERIALCOMPOSITION
REINFORCING FABRIC& IMPREGNATING RESIN
PLUS
\'ENGINEERED PROCESS\'
EQUALS
COMPOSITE LAMINATE WITH THE BEST WEIGHT TO STRENGTH PERFORMANCE
With respect to the raw materials selection -fabric and resin, the fabricating process and the and curing and test validation of composite part, these aspects must be carefully considered and in the engineering phase of the composite.
Step One:Fabric Selection
TYPESOF FABRIC WEAVE STYLE AND SURFACE FINISHINGFORRESIN TYPE COMPATIBILITY
Fabrics are generally considered ”balanced” if the breaking strength is within 15% warp to fill and are best in bias applications on lightweight structures.“Unbalanced” fabrics are excellent when a greater load is required one direction and a lesser load in the perpendicular direction.
- Tow: The bundle of individual carbon filaments used to weave carbon fabric. 50k tow means there are 48-50,000 carbon filaments in the tow. Smaller tow i.e. 12k, 6k, 3k, and 1k are obtained by dividing the 50k tow into smaller bundles.
- Thread Count: The number of threads (tow in carbon and yarn in Aramid) per inch. The first number will be the warp count and the second will be the fill count.
- Fill: The threads that run the width of the roll or bolt and perpendicular to the warp threads.
- Warp: The threads that run the length of the roll or bolt and perpendicular to the fill threads.Finish: The chemical treatment to fiberglass making it compatible with resin systems, therefore improving the bond between the fiber and the resin.
- Finishing fiberglass typically decreases the fiber strength by as much as 50%. Both Silane and Volan finishes are epoxy compatible. Historically, Volan has been considered a softer finish for a more pliable fabric, but recent advances have yielded some excellent soft Silane finishes.
- Thickness: Measured in fractions of an inch. The thicker the fabric the more resin required to fill the weave to obtain a surface-smooth finished part.
Weaves:
- Plain weave means the warp and fill threads cross alternately. This is the most common weave.
- 4 Harness (4 HS Satin or crowfoot) weave means the fill thread floats over three warp threads, then under one warp thread. This weave is more pliable than the plain weave, therefore conforms to complex curves more easily.
- 8 Harness (8 HS Satin) weave means the fill thread floats over seven warp threads, then under one warp thread. This weave is the most pliable of the standard fiberglass weaves.
- 2 x 2 Twill weave means the fill thread floats over two warp threads, then fewer than two warp threads. This weave is found most commonly in carbon fabrics and is more pliable than plain weave.
Most fabrics are stronger in the warp than the fill because higher tension is placed on the warp fiber keeping it straighter during the weaving process. Rare exceptions occur when a larger, therefore stronger thread is used in the fill direction than the warp direction.
PLAIN WEAVE
Isa verysimple weave pattern and the most common style. The warp and fill yarns are interlaced over and under each other in alternating fashion.Plain weave provides good stability, porosity and the least yarn slippage for a given yarn count.
8 HARNESS SATIN WEAVE
The eight-harness satin is similar to the four-harness satin except that one filling yarn floats over seven warp yarns and under one.
This is a very pliable weave and is used for forming over curved surfaces.
4 HARNESS SATIN WEAVE
The four-harness satin weave is more pliable than the plain weave and is easier to conform to curved surfaces typical in reinforced plastics. In this weave pattern, there is a three by one interfacing where a filling yarn floats over three warp yarns and under one.
2x2TWILL WEAVE
Twill weave is more pliable than the plain weave and has better drivability while maintaining more fabric stability than a four or eight harness satin weave. The weave pattern is characterized by a diagonal rib created by one warp yarn floating over at least two filling yarns.
SATINWEAVE TYPE CONFORMITYUNTO CURVED SHAPES
Plain Weaves, Bi-axial, Unidirectional StylesFor Directional High Strength PartsUse this weave style cloth when high strength parts are desired.It isidealfor reinforcement, mold making, aircraft andauto parts tooling,marine, and other composite lightweight applications.7544 Fiberglass - YouTube
FIBERGLASS FINISHING FOR RESIN COMPATIBILITY
All of the fiberglass fabrics is woven By HEXCEL COMPOSITES, a leading manufacturer of composite materials engineered for high-performance applications in marine, aerospace for commercial and military, automotive, sporting goods and other application-critical performance. These fabrics are 100% epoxy-compatible and will yield the bestmechanicalproperties when properly fabricated.
Finishing Cross ReferenceAndResin Type Compatibility
RESIN COMPATIBILITY
Burlington
Industries
Clark Schwebel
J.P Stevens
Uniglass Industries
Epoxy, Polyester
VOLAN A
VOLAN A
VOLAN A
VOLAN A
Epoxy, Polyester
I-550
CS-550
S-550
UM-550
Phenolic, Melamine
I-588
A1100
A1100
A1100
Epoxy, Polyimide
I-589
Z6040
S-920
UM-675
Epoxy
I-399
CS-272A
S-935
UM-702
Epoxy
CS-307
UM-718
Epoxy
CS-344
UM-724
Silicone
112
112
n-pH (neutral pH)
AVAILABLE FIBERGLASS, CARBON FIBER, AND KEVLAR FABRICS
HEXCEL 120 1.5-OUNCE FIBERGLASS PLAIN WEAVE 5 YARDS
HEXCEL 120 1.5-OUNCE FIBERGLASS PLAIN WEAVE 10 YARDS
HEXCEL 7532 7-OUNCE FIBERGLASS PLAIN WEAVE 5 YARDS
HEXCEL 1584 26 OUNCE FIBERGLASS SATIN WEAVE 3 YARDS
HEXCEL 1584 26 OUNCE FIBERGLASS SATIN WEAVE 5 YARDS
FIBERGLASS 45+/45- DOUBLE BIAS 3 YARDS
CARBON FIBER FABRIC 3K 2x2 TWILL WEAVE 6 OZ.3 YARDS
CARBON FIBER FABRIC 3K PLAIN WEAVE 6 OZ 3 YARDS
https://www..com/itm /311947292012
KEVLAR 49 HEXCEL 351 PLAIN WEAVE FABRIC 2.2 OZ
Step Two:Choose The Best Epoxy Resin SystemFor The ApplicationThe epoxy resinused infabricating a laminatewill dictate how theFRP will perform whenload or pressure is implied on the part. To choose the proper resin system, consider the following factorsthat are crucial to a laminate\'s performance. SIZE AND CONFIGURATION OF THE PART(NUMBER OF PLIES AND CONTOURED, FLATOR PROFILED)CONSOLIDATING FORCE(FREE STANDING DRY OR HAND LAY-UP, VACUUM BAG OR PLATEN PRESS CURING)CURING CAPABILITIES(HEAT CURED OR ROOM TEMPERATURE CURED)LOAD PARAMETERS(SHEARING FORCE, TORSIONAL AND DIRECTIONAL LOAD, BEAM STRENGTH)ENVIRONMENTAL EXPOSURE
The principal role of the resin is to bind thefabric into ahomogeneousrigidsubstrate(OPERATING TEMPERATURE, AMBIENT CONDITIONS, CHEMICAL EXPOSURE, CYCLIC FORCE LOADING)MATERIAL AND PRODUCTION COST(BUYING IN BULK WILL ALWAYS PROVIDE THE BEST OVERALL COSTS)
These factors will dictate the design and the composition of the part and must be carefully considered during the design and engineering phase of the fabrication.
TOP SELLING IMPREGNATING RESIN SYSTEMThe following resin systems have been used as impregnating resin for composites fabrics (Fiberglass, Cabon Fiber, Kevlar, etc.).Each resin was formulated specifically to the high-lighted application and demonstrates excellent performance based on the intended use.
MAX BOND LOW VISCOSITY A/B
Marine GradeBoatBuildingResin System, Fiberglassing/Impregnating, Water Resistance, Cured Structural Strength
MAX BOND LOW VISCOSITY 32-Ounce kit
MAX BOND LOW VISCOSITY 64-Ounce Kit
MAX BOND LOW VISCOSITY 1-Gallon Kit
MAX BOND LOW VISCOSITY 2-Gallon Kit
MAX BOND LOW VISCOSITY 10-Gallon Kit
MAX 1618 A/B
Crystal Clear, High Strength, Lowest Viscosity (Thin), Durability & Toughness, Excellent Wood Working Resin
MAX 1618 A/B 48-Ounce Kit
MAX 1618 A/B 3/4-Gallon Kit
MAX 1618 A/B 3/4-Gallon Kit
MAX 1618 A/B 1.5-Gallon Kit
MAX CLR A/B
Water Clear Transparency, Chemical Resistance, FDA Compliant For Food Contact, High Impact, Low Viscosity
MAX CLR A/B 24-Ounce Kit
MAX CLR A/B 48-Ounce Kit
MAX CLR A/B 96-Ounce Kit
MAX CLR A/B 96-Ounce Kit
MAX CLR A/B 1.5-Gallon Kit
MAX GRE A/B
GASOLINE RESISTANT EPOXY RESIN
Resistant To Gasoline/E85 Blend, Acids & Bases, Sealing, Coating, Impregnating Resin
MAX GRE A/B 48-Ounce Kit
MAX GRE A/B 96-Ounce Kit
MAXHTEA/B
HIGH-TEMPERATURE EPOXY
Heat Cured Resin System For Temperature Resistant Bonding, Electronic Potting, Coating, Bonding
MAX HTE A/B 80-Ounce Kit
MAX HTE A/B 40-Ounce Kit
Proper Lay-Up Technique -Putting It All Together
Pre-lay-up notes
- Lay out the fabric and pre-cut to size and set aside
- Avoid distorting the weave pattern as much as possible
- For fiberglass molding, ensure the mold is clean and adequate mold release is used
- View our video presentation above \"MAX EPOXY RESIN MIXING TECHNIQUE\"
- Mix the resin only when all needed materials and implements needed are ready and within reach
Mix the proper amount of resin needed and be accurate proportioning the resin and curing agent.Adding more curing agent than the recommended mix ratio will not promote a faster cure.Over saturation or starving the fiberglass or any composite fabric will yield poor mechanical performance. When mechanical load or pressure is applied to the composite laminate, the physical strength of the fabric should bear the stress and not the resin. If the laminate is over saturated with the resin it will most likely to fracture or shatter instead of rebounding and resist damage.
Don’t how much resin to use to go with the fiberglass?
A good rule of thumb is to maintain a minimum of 30 to 35% resin content by weight, this is the optimum ratio used in high-performance prepreg (or pre-impregnated fabrics) typically used in aerospace and high-performance structural application.
For general hand lay-ups, calculate using 60% fabric weight to 40% resin weight as a safety factor. This will ensure that the fabricated laminate will be below 40% resin content depending on the waste factor accrued during fabrication.
Place the entire pre-cut fiberglass to be used on a digital scale to determine the fabric to resin weight ratio.Measuring by weight will ensure accurate composite fabrication and repeatability, rather than using OSY data.
THE USE OF A WEIGHING SCALE IS HIGHLYRECOMMENDED
Purchase this scale with any of ourproduct offering and the shipping cost of the scale is free.
A good rule of thumb is to maintain a minimum of 30 to 35% resin content by weight, this is the optimum ratio used in high-performance prepreg (or pre-impregnated fabrics) typically used in aerospace and high-performance structural application. For general hand lay-ups, calculate using 60% fabric weight to 40% resin weight as a safety factor. This will ensure that the fabricated laminate will be below 40% resin content depending on the waste factor accrued during fabrication.
Place the entire pre-cut fiberglass to be used on a digital scale to determine the fabric to resin weight ratio. Measuring by weight will ensure accurate composite fabrication and repeatability, rather than using OSY data.
Typical fabric weight regardless of the weave pattern
1 ounce per square yard is equal to 28.35 grams
1 square yard equals to 1296 square inches (36 inches x 36 inches)
FOR EXAMPLE
1 yard of 8-ounces per square yard (OSY) fabric weighs 226 grams
1 yard of 10-ounces per square yard (OSY) fabric weighs 283 grams
Ounces per square yard or OSY is also known as aerial weight, which is the most common unit of measurement for composite fabrics.To determine how much resin is needed to adequately impregnate the fiberglass, use the following equation:
(Total Weight of Fabric divided by 60%)X( 40%)= weight of mixed resin needed
OR
fw= fabric weight
rc= target resin content
rn=resin needed
MASTER EQUATION
(fw/60%)x(40%)=rn
FOR EXAMPLE
1 SQUARE YARD OF 8-OSY FIBERGLASS FABRIC WEIGHS 226 GRAMS
(226 grams of dry fiberglass / 60%) X 40% = 150.66 grams of resin needed
So for every square yard of 8-ounce fabric, itwill need 150.66 grams of mixed resin.
Computing For Resin And Curing Agent Amount
150.66 grams of resin needed
MIX RATIO OF RESIN SYSTEM IS 2:1 OR
50 PHR (per hundred resin)
2 = 66.67% (2/3)
+
1 = 33.33%(1/3)
=
(2+1)=3 or (66.67%+33.33%)=100% or (2/3+1/3)= 3/3
150.66 x 66.67%= 100.45 grams of Part A RESIN
150.66 x 33.33%= 50.21 grams of Part B CURING AGENT
100.45 + 50.21 = 150.66 A/B MIXTURE
GENERAL LAY-UP PROCEDURE
Apply the mixed resin onto the surface and then lay the fabric and allow the resin to saturate through the fabric.
NOT THE OTHER WAY AROUND
This is one of the most common processing error that yields sub-standard laminates.By laying the fiberglass onto a layer of the prepared resin, fewer air bubbles are entrappedduring the wetting-out stage.Air is pushed up and outwards instead of forcing the resin through the fabric which will entrap air bubbles. This technique will displace air pockets unhindered and uniformly disperse the impregnating resin throughout the fiberglass.
HAND LAY-UP TECHNIQUE
Eliminating air entrapment or void porosity in an epoxy/fiberglass lay-up process
Fiberglass Hand Lay Up For Canoe and Kayak Building- Cedar Strip Kayak Fiberglassing - YouTube
Video will open in a new window
Basic Hand Lay-up Fiberglassing
Video will open in a new window
VACUUM BAGGING PROCESSFor performance critical application used in aerospace vehicles, composite framing for automotive vehicles and marine vessels, a process called \'Vacuum Bagging\' is employed to ensure the complete consolidation of every layer of fabric.The entire tooling and lay-up are encased in an airtight envelope or bagging and a high-efficiency vacuum pump is used to draw out the air within the vacuum bag to create negative atmospheric pressure. Once a full vacuum (29.9 Inches of Mercury) is achieved, the negative pressure applies a compacting force of 14.4 pounds per square inch (maximum vacuum pressure at sea level) is applied to the vacuum bag transferring the force to the entire surface area of the laminate.
Vacuum pressure is maintained until the resin cures to a solid. For room temperature curing resin system, the vacuum pump is left in operation for a minimum of 18 hours. External heat can be applied to the entire lay-up, thus accelerating the cure of the resin system.
The vacuum force also removes any entrapped air bubble between the layers of fabric and eliminate what is called, porosity or air voids. Porosity within a laminate creates weak spots in the structure that can be the source of mechanical failure when force or load is applied to the laminate.
Thestandard atmosphere(symbol: atm) is aunit of pressuredefined as101325Pa(1.01325bar), equivalent to760mm Mercury or29.92inches Mercury or14.696pounds per square inch of pressure.
FiberglaSs And Carbon Fiber Vacuum Bagging and Flat Panel Laminate - YouTube
Video will open in a new window
AUTOCLAVE CURING PROCESSBASIC OPERATION OF THE AUTOCLAVE PROCESS
In the autoclave process, high pressure and heat are applied to the part through the autoclave atmosphere, with a vacuum bag used to apply additional pressure and protect the laminate from the autoclave gases.The cure cycle for a specific application is usually determined empirically and, as a result, several cure cycles may be developed for a single material system, to account for differences in laminate thickness or to optimize particular properties in the cured part. The typical autoclave cure cycle is a two-step process. First, vacuum and pressure are applied while the temperature is ramped up to an intermediate level and held there for a short period of time. The heat reduces the resin viscosity, allowing it to flow and making it easier for trapped air and volatiles to escape. The resin also begins wetting the fibers at this stage.In the second ramp up, the temperature is raised to the final cure temperature and held for a sufficient length of time to complete the cure reaction. During this step, the viscosity continues to drop, but preset temperature ramp rates and hold times then stabilize viscosity at a level that permits adequate consolidation and fiber wetting, while avoiding excessive flow and subsequent resin starvation.These control factors also slow the reaction rate, which prevents excessive heat generation from the exothermic polymerization process.Upon completion, the cured mechanical performance of the composite is often much stronger and lighter compared to a hand lay-up, or vacuum bagged composite laminate.
VACUUM INFUSION PROCESSVacuum Infusion Process is also known in the composites industry asVacuum Assisted Resin Transfer Molding or VARTM.
Similar to the Vacuum Bagging Process where the negative pressure is used to apply consolidation force to the laminate while the resin cures, the resin is infused into the fabric lay-up by sucking the impregnating resin and thus forming the composite laminate.
The VARTM Process produces parts that require less secondary steps, such as trimming, polishing or grinding with excellent mechanical properties. However, vacuum infusion requires more additional or supplemental related equipment and expendable materials. So the pros and cons of each presented composite fabrication process should be carefullydeterminedto suit the user\'scapabilitiesand needs.
Please view the following video demonstration which explains the process of Vacuum Infusion or VARTM process.
MAX 1618 A/B VACUUM ASSISTED RESIN TRANSFER MOLDING PROCESS
CARBON FIBER VACUUM INFUSION WITH EPOXY RESIN - VACUUM BAGGING WITH MAX 1618 EPOXY RESIN - YouTube
Video will open in a new window
Step Four: Proper CuringAlthough we have formulated all of ur MAX EPOXY RESIN SYSTEM product line to be resistant to amine-blush, it isrecommendednot to mixany resin systems in high humidity conditions, greater than 60%. Always make sure that the substrate or material the epoxy resin system is being applied to is well preparedas possible to ensure the best-cured performance.Always review the published data and information for proper usage, application, and general safety information.
Our expert staff of engineers isalways available forconsultationand assistance.
Allow the lay-up to cure for a minimum of 24 to 36 hours before handling. Optimum cured propertiescan take up to 7 days depending on the ambient cure condition.The ideal temperature cure condition of most room temperature epoxy resin is 22 to 27 degrees Celsius at 20% relative humidity. Higher ambient curing temperatures will promote faster polymerization and development of cured mechanical properties. Improving mechanicalperformance via post heat cureA short heat post cure will further improve the mechanical performance of most epoxy resins. Allow the applied resin system to cure at room temperature until for 18 to 24 hours and if possible, expose heat cure it in an oven or other sources of radiant heat (220°F to 250°F) for 45 minute to an hour. You can also expose it to direct sunlight but place a dark colored cover, such as a tarp or cardboard to protect it from ultraviolet exposure. In general room temperature cured epoxy resin has a maximum operating temperature of 160°For lower. A short heat post cure will ensure thatthemixed epoxysystem is fully cured,especiallyfor room temperature cure system that can take up to 7 days toachieve 100% cure.Some darkening or yellowing of the epoxy resin may occurif overexposed tohigh temperature (>250 F).
AMINE BLUSHThe affinity ofan amine compound (curing agent) to moisture and carbon dioxide creates a carbonate compoundand forms what is called amine blush.Amine blush is a wax-like layer that forms as most epoxies cure. If the epoxy system is cured in extreme humidity (>70%).It will be seenas awhite and waxy layer that must be removed byphysical sanding of the surface followed by an acetone wipe.
TESTING THE COMPOSITEDetermination Of The Fabric-Resin Ratio
TESTING FABRIC TO RESIN RATIO VIA RESIN BURN OUT - YouTube
Video will open in a new window
UltimateCompressive Strength
ULTIMATE COMPRESSIVE STRENGTH TEST
Video will open in a new window
6500 Pounds Load / 0.498 square inch = 13,052 psi Maximum Compressive Strength
SPECIMEN EXAMINATION AFTER COMPRESSION TEST - YouTube
Video will open in a new window
DON\'T FORGET OUR EPOXY MIXING KIT
Click The Link To Add To class=\"MsoNormal\" align=\"center\" style=\"font-size: 14pt;\">
EVERYTHING YOU NEED TOMEASURE, MIX, DISPENSE OR APPLY
Click The Link To Add To the correct amount is equally as importantto attain the intended cured properties of the resin system.The container in which the epoxy and curing agent is mixed is an important consideration when mixing an epoxy resin system.The container must withstand the tenacity of the chemical and must be free of contamination.Most epoxy curing agent has a degree of corrosivity, as a general practice, protective gloves should be wornwhen handling chemicals of the same nature.
MIXING KIT CONTENTS
1 Each Digital Scale -Durable, Accurate Up To 2000.0 Grams
4 Each 32-ounce (1 Quart) Clear HDPE Plastic Mix Cups
4 Each 16-ounce (1 Pint) Clear HDPE Plastic Mix Cups
5 Pairs One Size Fits All Powder-Free Latex Gloves
2 Each Graduated Syringes
Wooden Stir Sticks
Foam Brush
IMPORTANT NOTICE
Your purchase constitutes the acceptance of this disclaimer. Please review before purchasing this product.
The user should thoroughly test any proposed use of this product and independently conclude the satisfactory performance in the application. Likewise, if the manner in which this product is used requires government approval or clearance, the user must obtain said approval.
The information contained herein is based on data believed to be accurate at the time of publication. Data and parameters cited have been obtained through published information, PolymerProducts and Polymer Composites Inc. laboratories using materials under controlled conditions. Data of this type should not be used for a specification for fabrication and design. It is the user\'s responsibility to determine this Composites fitness for use.
There is no warranty of merchantability for fitness of use, nor any other express implied warranty. The user\'s exclusive remedy and the manufacturer\'s liability are limited to refund of the purchase price or replacement of the product within the agreed warranty period.PolymerProducts and its direct representative will not be liable for incidental or consequential damages of any kind.Determination of the suitability of any kind of information or product for the use contemplated by the user, the manner of that use and whether there is any infringement of patents is the sole liability of the user.