When you click on links to various merchants on this site and make a purchase, this can result in this site earning a commission. Affiliate programs and affiliations include, but are not limited to, the eBay Partner Network.
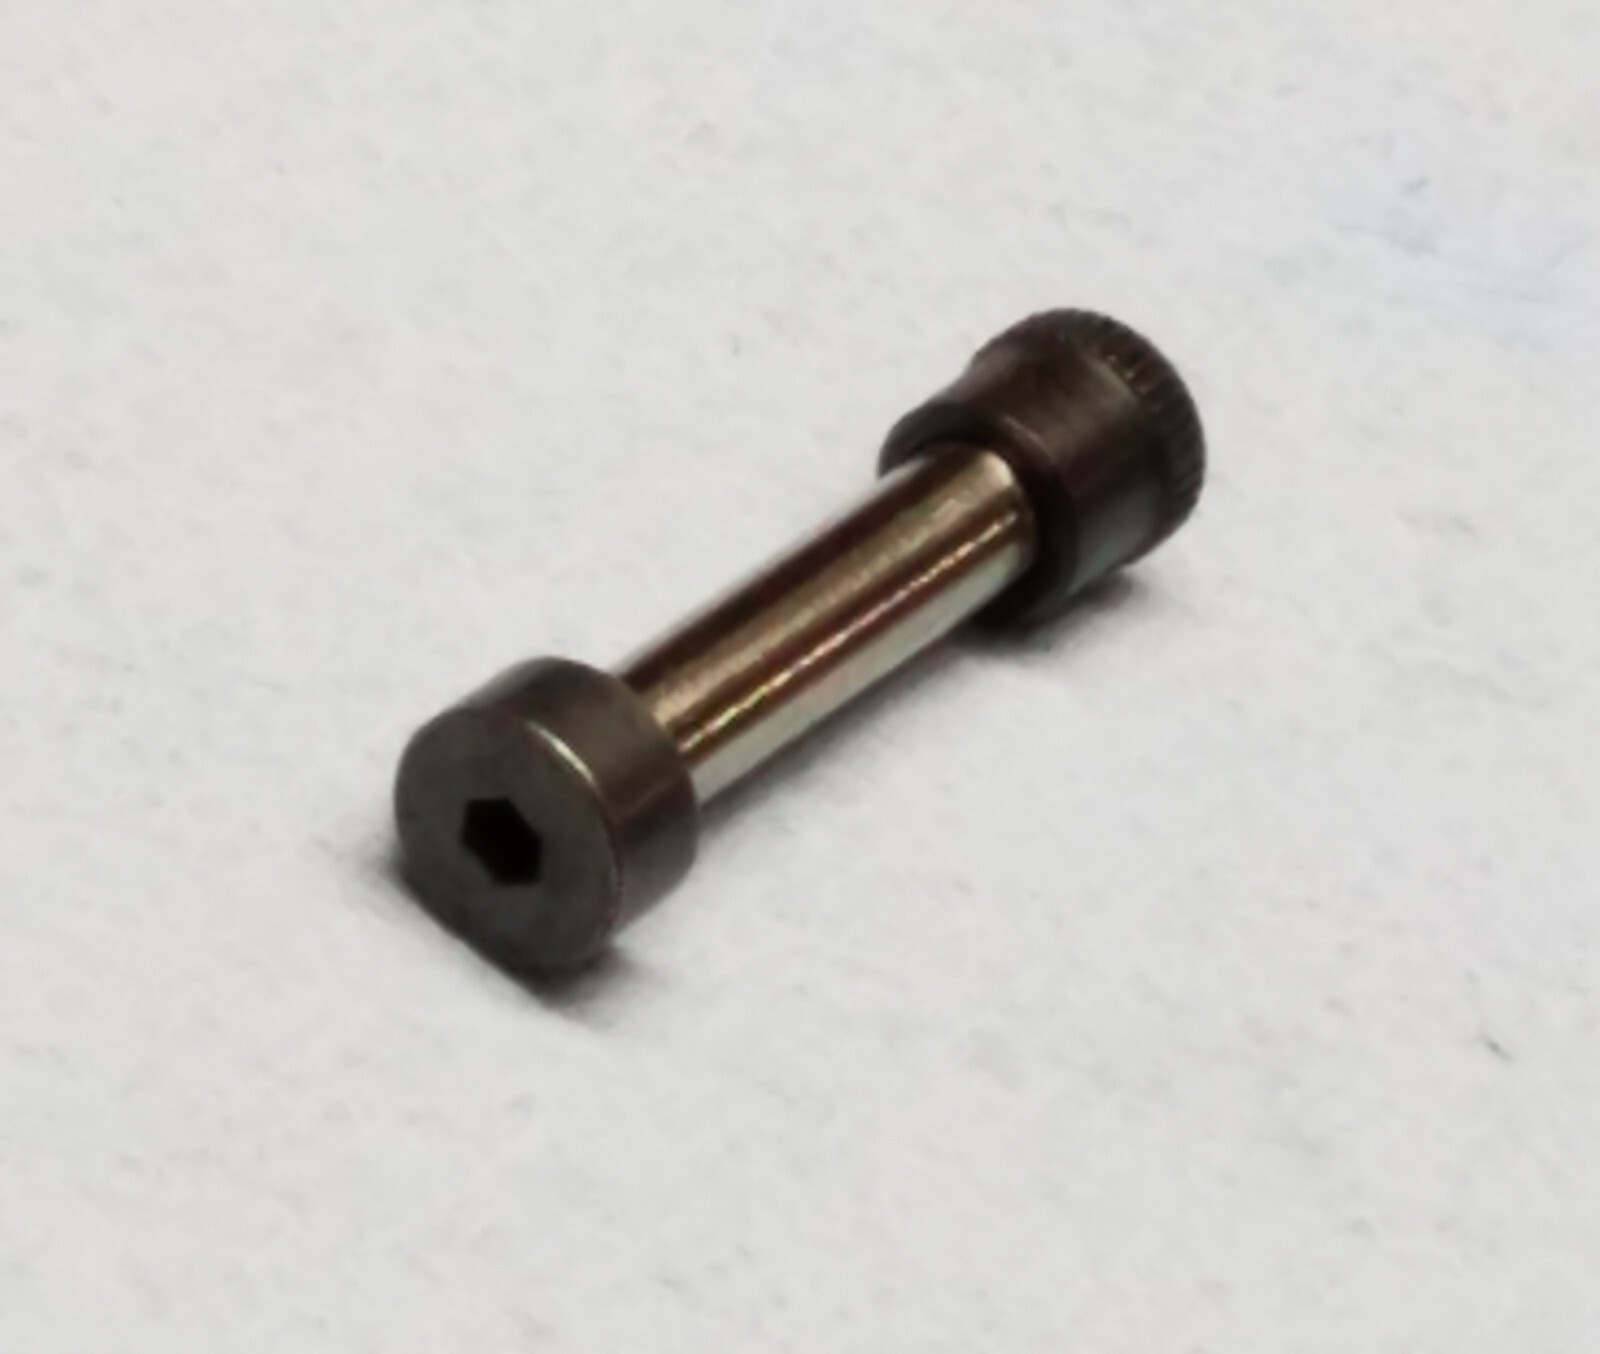
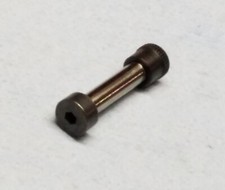
This listing complies with \'s air gun guidelines found here and I will only sell and ship air guns to buyers in jurisdictions where permitted by applicable laws - listing is for one custom pivot pin with nut, other parts shown for reference only.
FITS THE CURRENT CHINESE-MADE MODELS PERFECTLY, FOR THE OLDER USA-MADE MODELS PLEASE READ THE NOTES AND INSTRUCTIONS BELOW, THIS PART REQUIRES FITTING FOR USA MODELS
This two-piece pin is made of super-strong grade 12 alloy steel. The pin fits a 3/32\" hex, the 12-point socket of the nut fits a 3/16\" hex wrench, no hex wrenches or other tools included. These parts have a durable black-oxide finish, the pin-shaft is polished raw steel. The pin has a shoulder that stops the nut at 3/4\" which is the same as the outside tube diameter, this prevents the front of the tube from expanding when force is applied to the pump-lever and also prevents over-compressing the front of the tube. This is the strongest and most stable pin design available in the industry.
IMPORTANT, the following two paragraphs are critical for installing a solid pivot-pin :
The hole in the unmodified factory USA tube is 3/16\" slip-fit on the left side and 3/16\" press-fit on the right side. This solid pin requires a 3/16\" slip-fit on both sides. A standard 3/16\" drill bit can be used to enlarge the hole to the correct size. The hole on the left side is usually large enough to fit the drill bit to line up straight with the right side to keep them aligned correctly. The sharp edges of the holes inside the tube should be deburred after drilling to avoid damaging the valve and piston seals. This can be done with a small round hobby file or a 2\" x 2\" piece of 300-400 grit sandpaper rolled tightly into a tube to use as a file. Insert the file through the outside of the hole at an angle and file lightly around the inside edge until it is dull all the way around, do this to both holes, then file or sand the inside surface around the holes reaching in from the front of the tube to make sure everything is smooth. Do not remove a lot of metal, just enough to dull the sharp edge and smooth the internal area around the holes.
Some tubes have the pivot-pin holes further back than others. Older tubes tended to have them closer to the front of the tube, newer tubes tend to have them back further which causes the barrel band holes to be slightly off-center (too far forward) for the pivot pin to fit through easily. With the factory roll-pin you can simply force the pin through and it will compress to fit. With this solid pin you may have to file the front of the tube back slightly until the holes align. This is very easy to do, only a few file strokes are needed in most cases, a few dozen in other cases. Be very careful to keep filings out of the tube where they can cause damage to the seals and valve, stuffing a piece of rag into the tube before starting this work and removing it afterwards helps keep filings and grit out of the tube, flushing the tube out with rubbing alcohol is a good idea also, the best way is to remove all parts from the tube so it can be cleaned and reassembled correctly afterwards.